Case Studies

Upgrade & Process Optimisation


Background
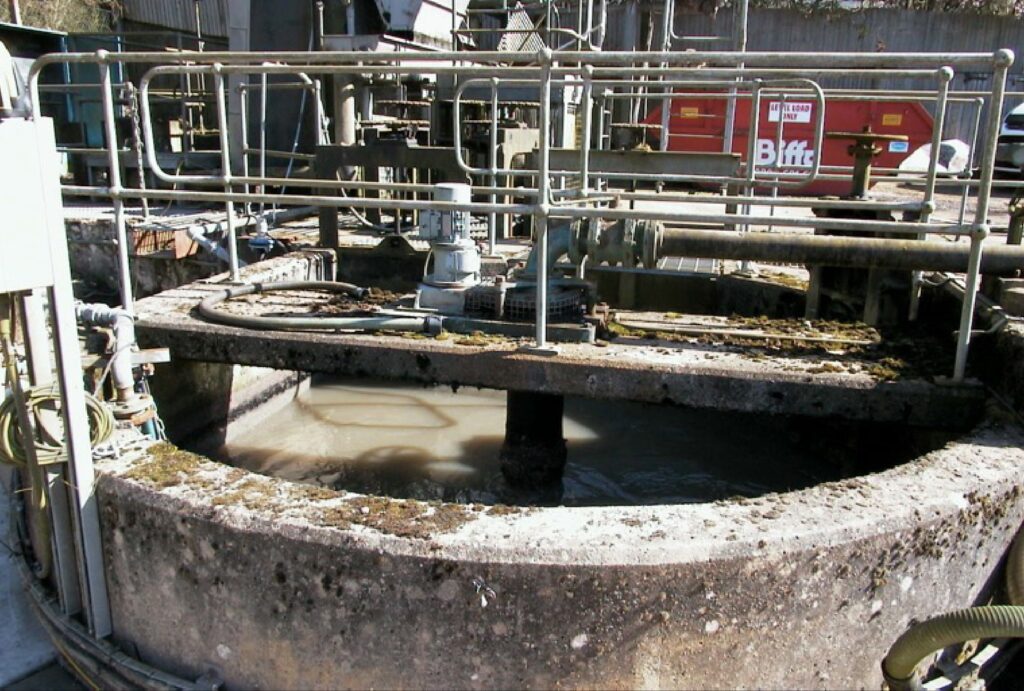
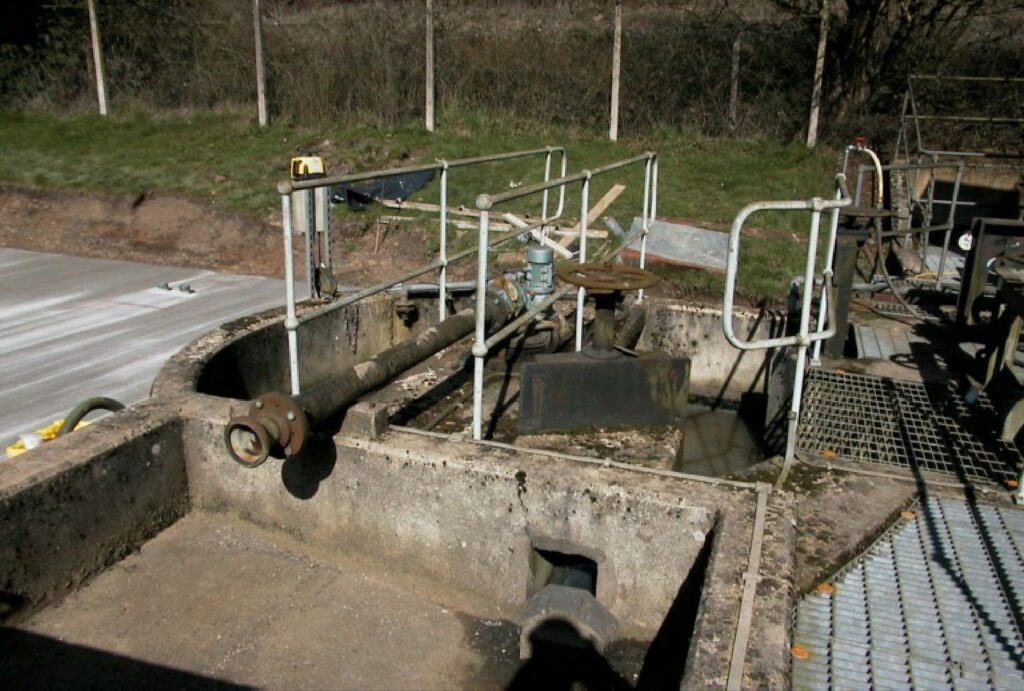
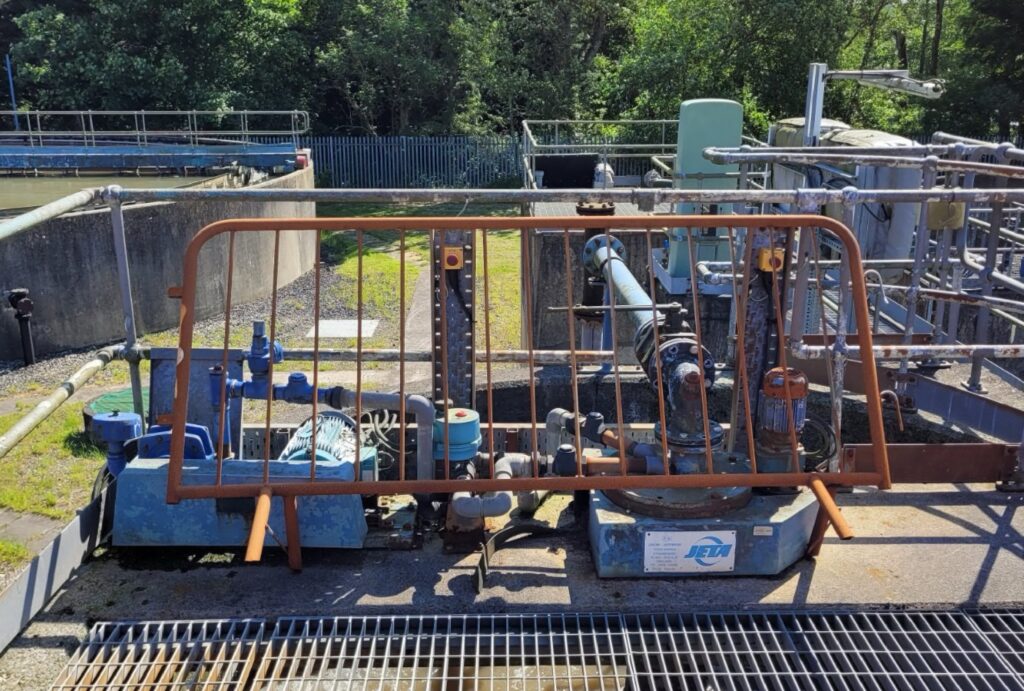
Existing grit removal system was at end of service life, causing poor grit capture, sediment build-up, high maintenance demands, and increased downstream equipment wear.

Existing Issues 

  • Severely deteriorated chambers and mechanical equipment
  • Frequent manual cleaning required
  • Increasing labour, downtime, and safety risks

Solution 
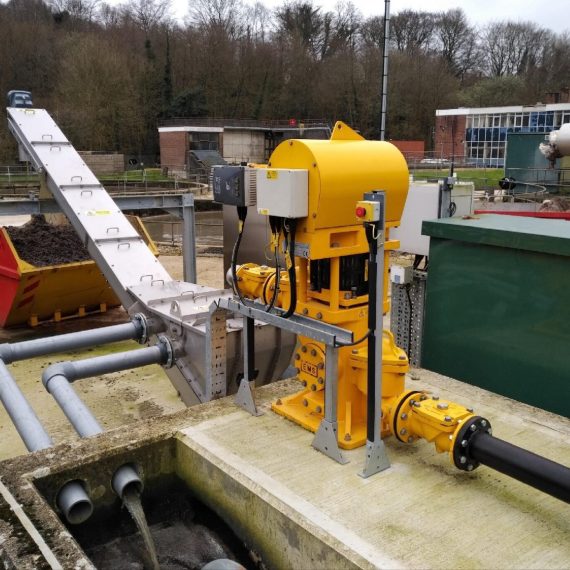
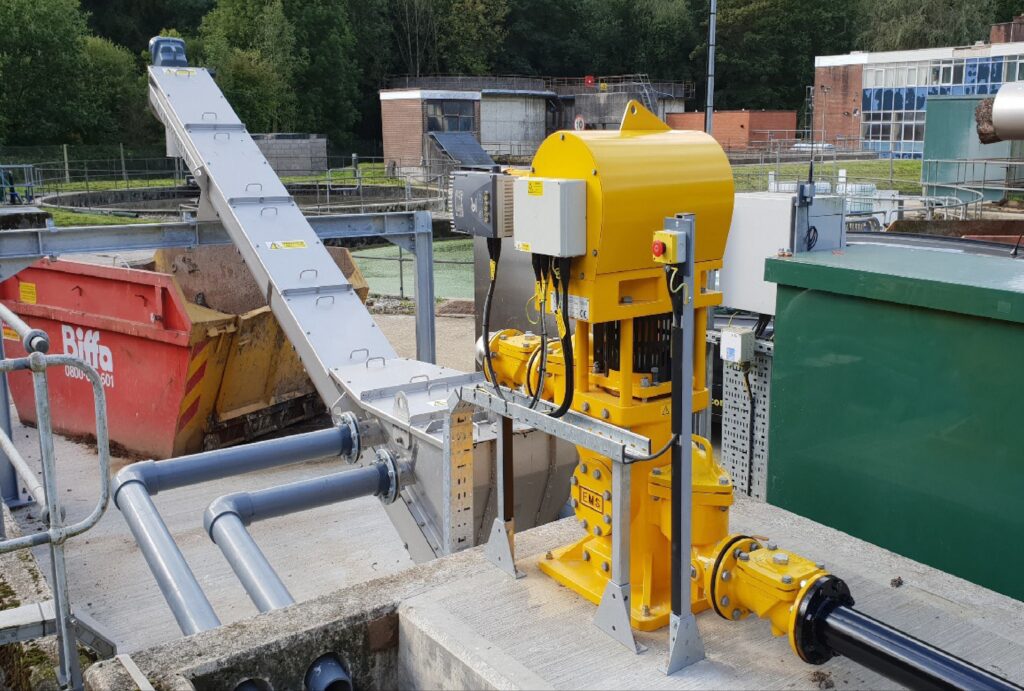
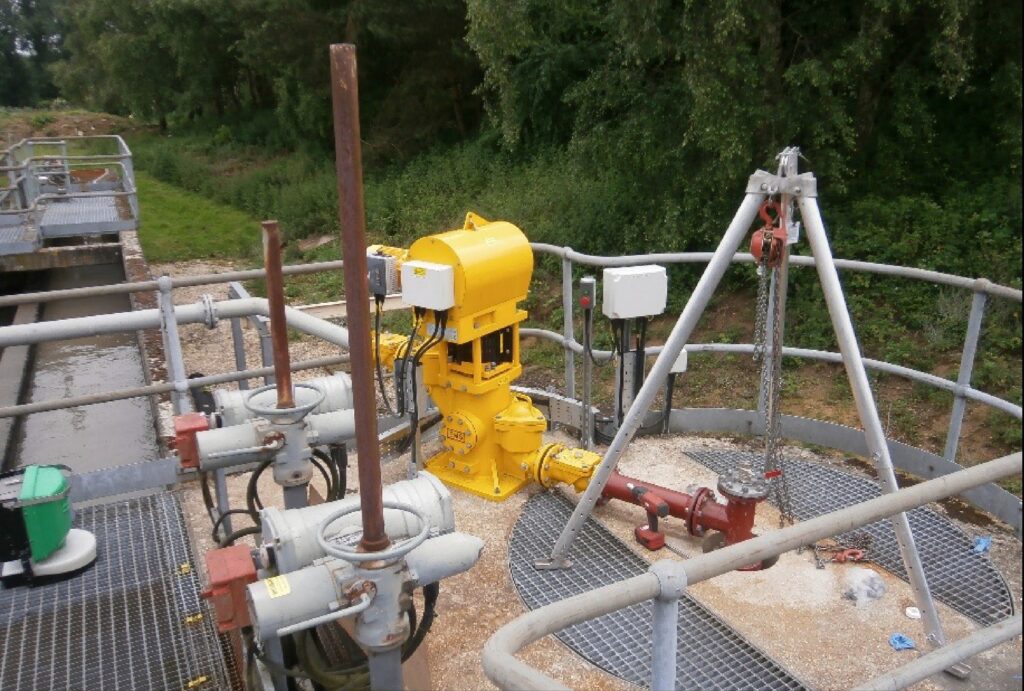
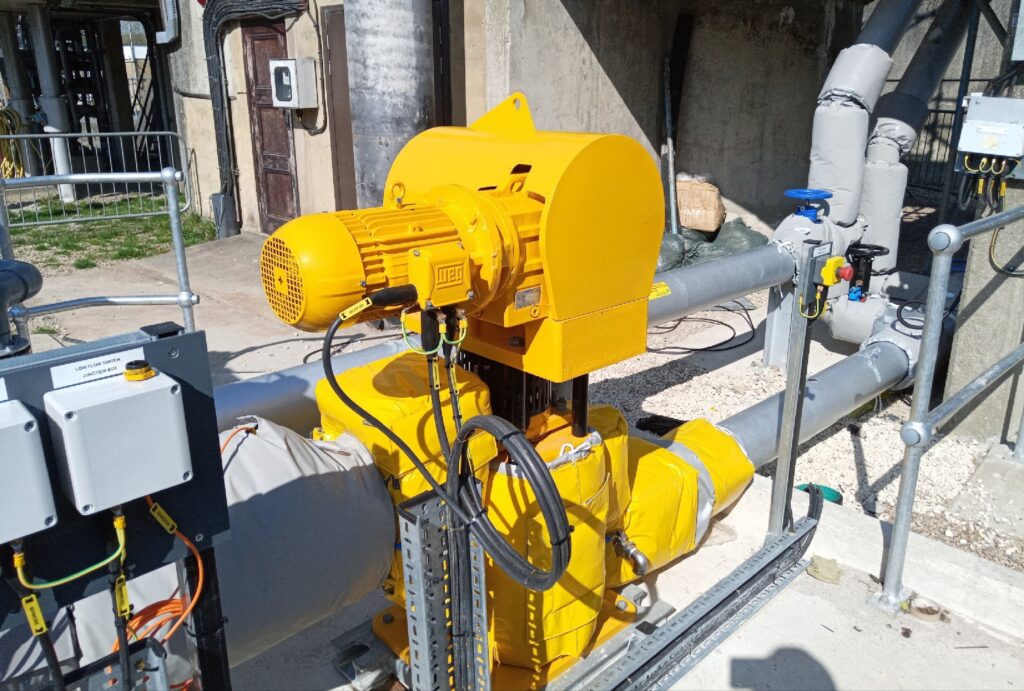
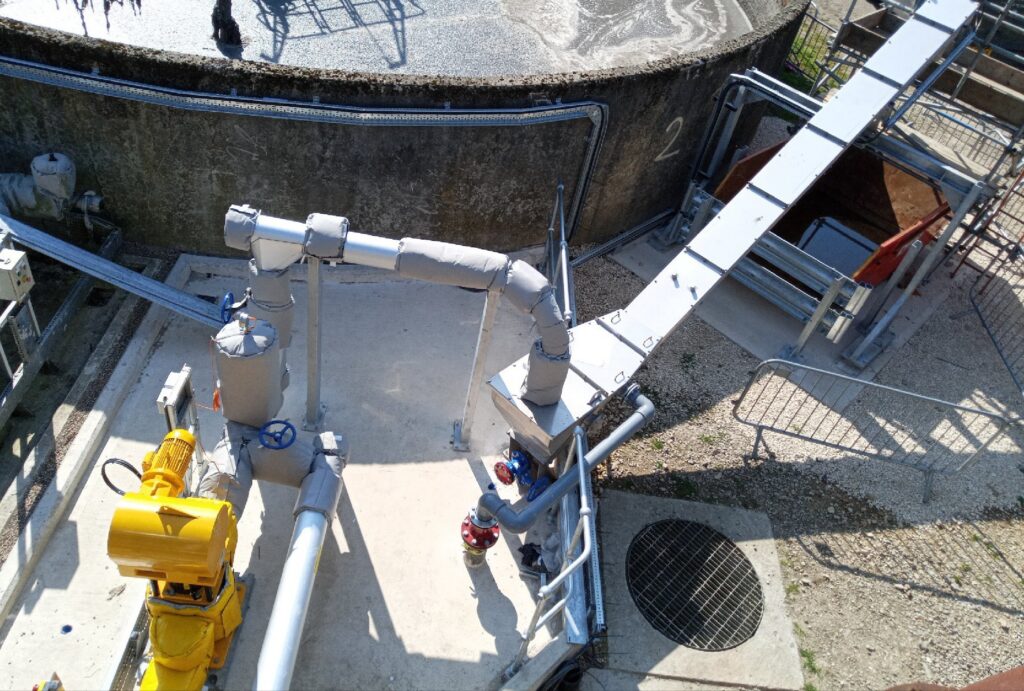
Installation of a modern grit removal system centred around an EMS Ram Pump, aligned with GRS strategy for durability, reliability, and low maintenance.

Additional Upgrades
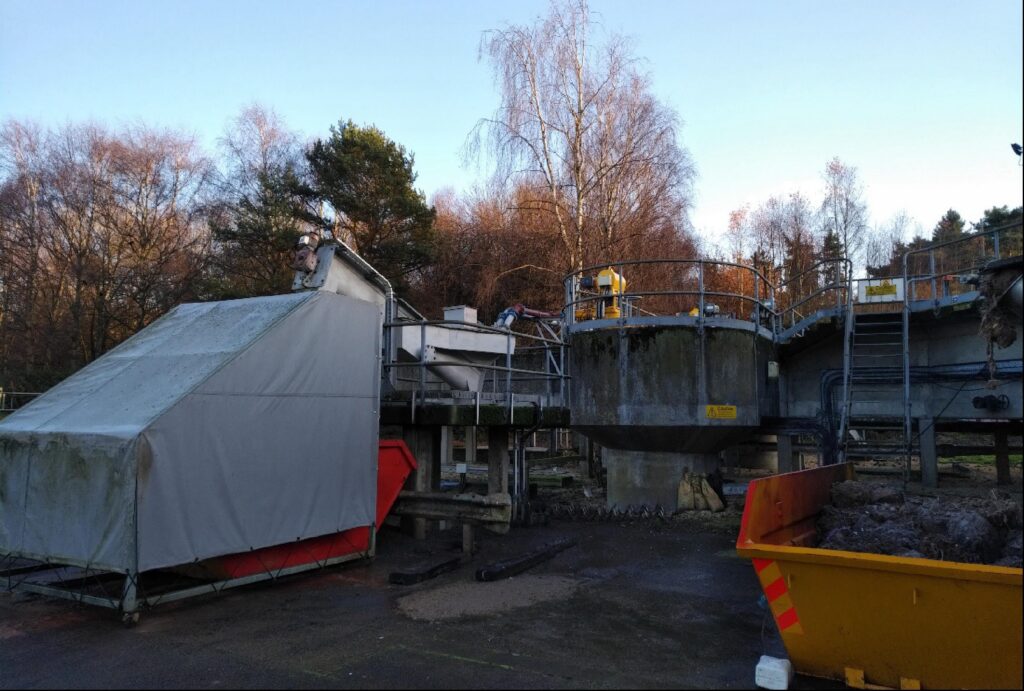
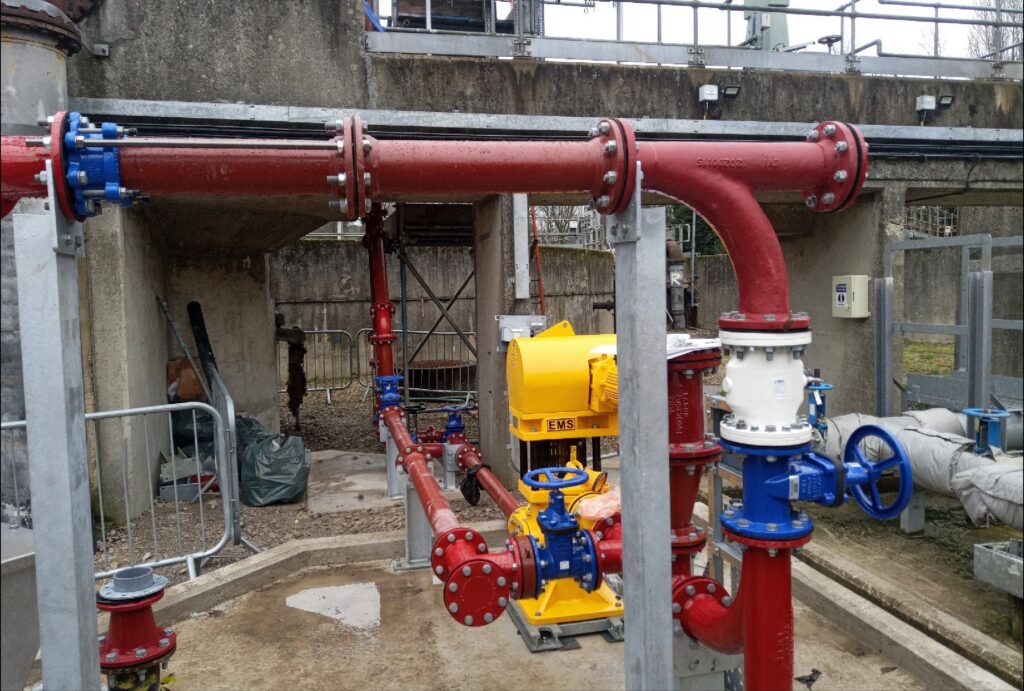
The scope of works included the installation of a new grit classifier to improve grit separation and washing efficiency. New discharge pipework, valves, and a custom suction hose were also installed to enhance system performance and reliability. In addition, electrical controls and emergency stop systems were upgraded to support improved automation, operational control, and site safety.

Installation & Integration
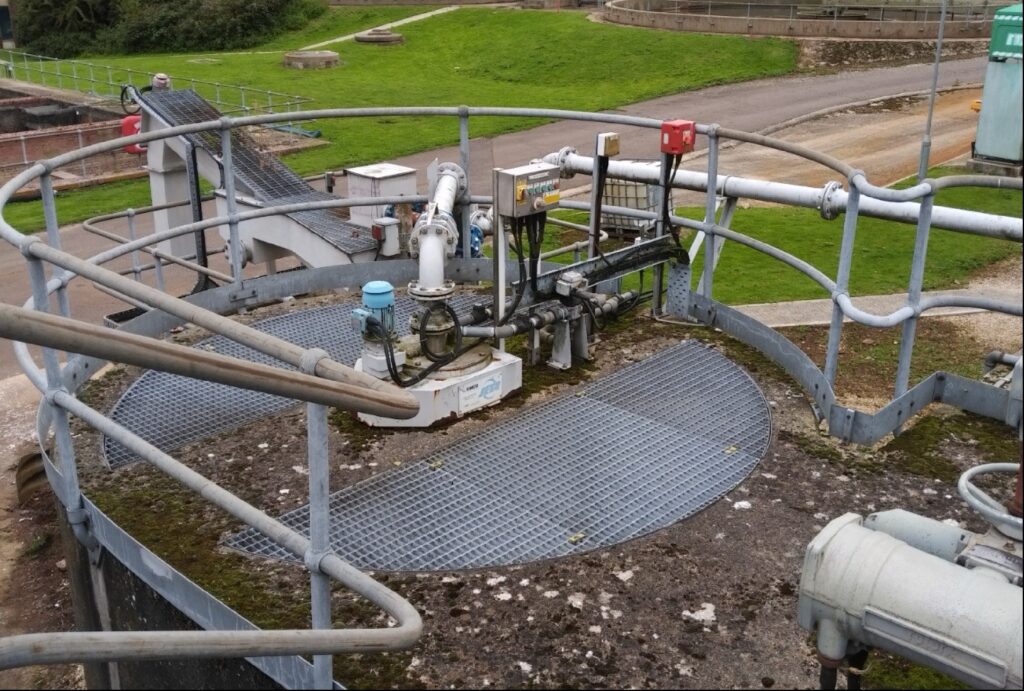
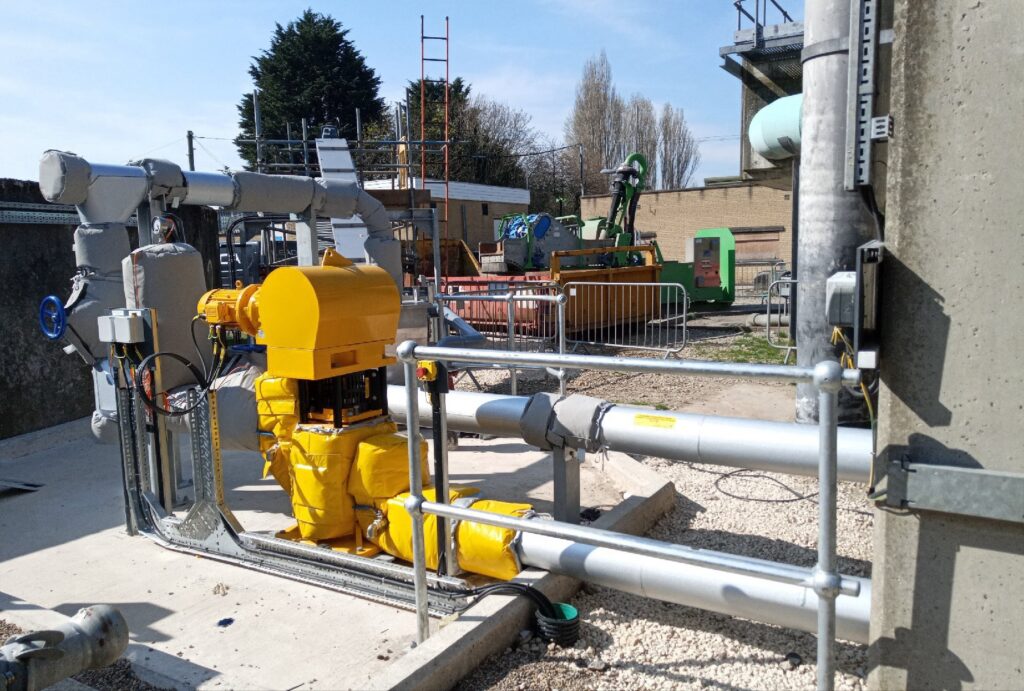
All new equipment was installed within the existing grit chamber footprint, minimising the need for civil modifications and reducing both project cost and operational disruption. Proven, corrosion-resistant equipment was selected to ensure long-term reliability in the harsh wastewater environment. Electrical and control systems were fully integrated with the existing site infrastructure to enable automated operation. The EMS CVR200 Ram Pump was selected specifically to accommodate the site’s variable flow conditions.

Results & Benefits
Following commissioning, the upgraded system delivered a significant improvement in grit capture and removal efficiency. The EMS Ram Pump provided reliable grit pumping with minimal maintenance requirements, reducing unplanned downtime. Improved grit removal reduced carryover to downstream processes, lowering equipment wear and ongoing maintenance costs. Operator safety was enhanced through increased automation, improved access, and upgraded guarding.

GRS Strategy Outcomes
The upgraded system aligns fully with GRS strategy principles. Reliability was improved through the use of robust, long-life equipment. Efficiency gains were achieved by reducing operational and maintenance costs. Safety was enhanced by minimising manual intervention and improving working conditions. Sustainability objectives were met through the reuse of existing infrastructure, reducing both environmental impact and capital expenditure.

Conclusion
The grit removal upgrade delivered a future-proof, resilient solution that transformed an aging process into a reliable and efficient system. The project extended asset life, improved operational performance and safety, and provides long-term protection for downstream treatment processes.

Targeted Pump Replacement & Efficiency Enhancement

Background
Recurring failures of the existing grit pump were causing unreliable grit handling, despite the classifier and pipework remaining in good condition. A targeted pump replacement was identified as the most cost-effective solution aligned with GRS strategy principles.

Existing Issues 

  • Reduced pumping efficiency due to impeller erosion
  • Frequent blockages during peak grit loads
  • High maintenance demand and reactive interventions
  • Increased downstream wear from incomplete grit removal

Solution
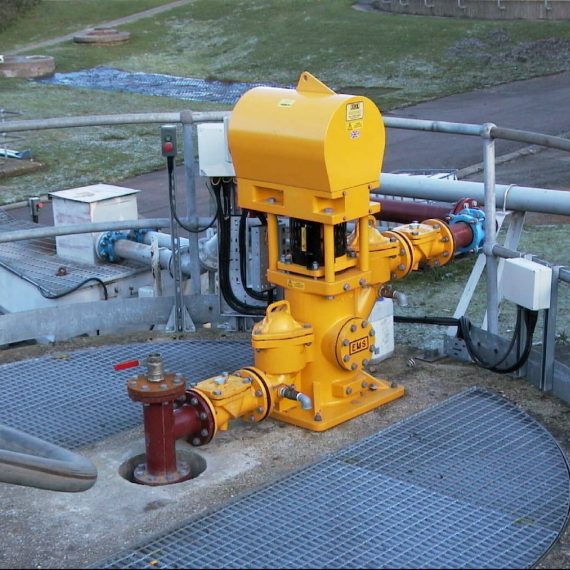
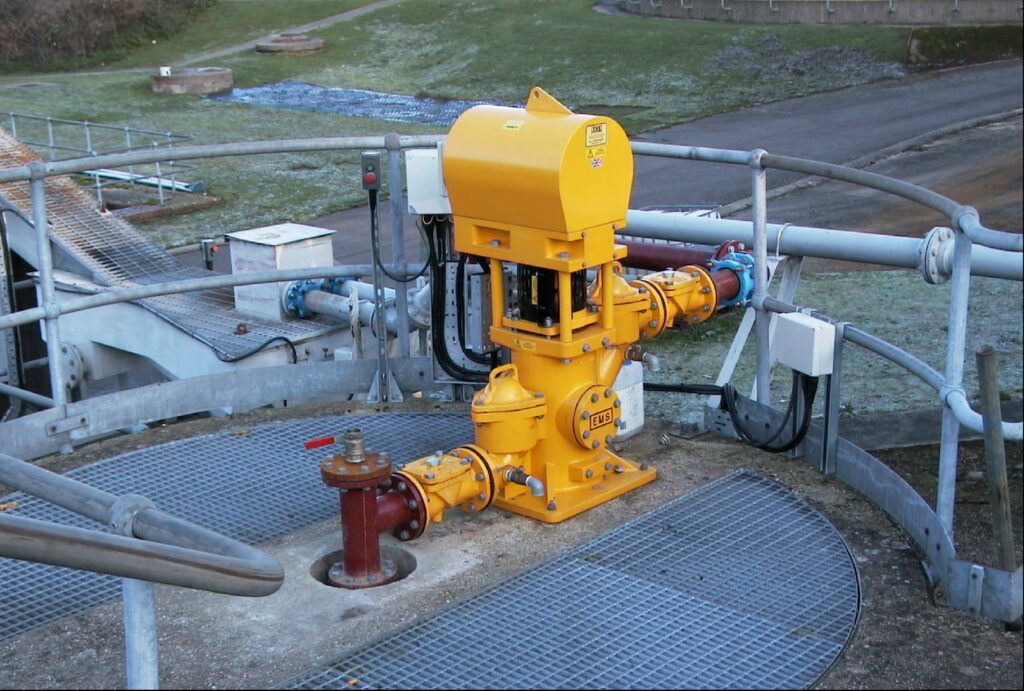
The upgrade focused on replacing the existing grit pump with an EMS CVR200 Ram Pump while retaining all downstream grit-handling infrastructure. This targeted approach minimised capital cost, reduced waste, and avoided unnecessary disruption to the site, while restoring reliable grit transfer performance.

Why EMS CVR200
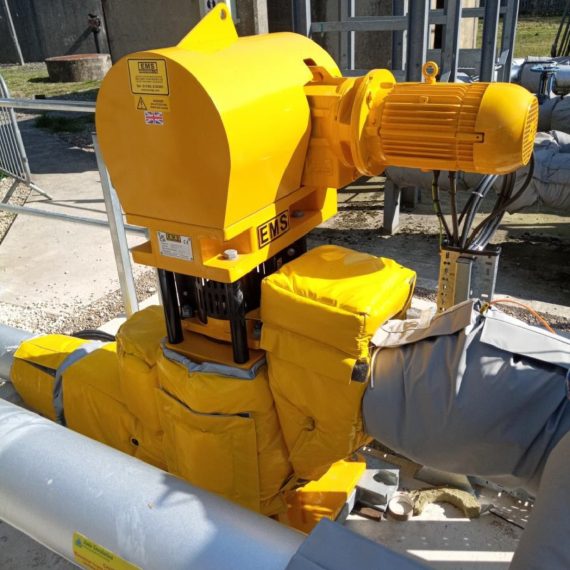
The EMS CVR200 Ram Pump was selected for its proven suitability in handling high specific-gravity, abrasive grit slurries. Its adjustable stroke rate allows the pump to respond effectively to variable influent flow conditions. The pump’s abrasion-resistant construction, combined with replaceable wear components, ensures long service life in demanding environments. A low-speed, high-torque ram drive eliminates the need for impellers and other high-wear rotating parts, significantly reducing maintenance. The vertical, top-mounted configuration makes the CVR200 particularly well suited to retrofit installations, with minimal ongoing maintenance requirements.

Installation & Integration
The CVR200 was installed directly on the existing grit chamber footprint, removing the need for civil modifications. Hydraulic integration with the existing classifier and pipework was seamless, ensuring continuity of operation. This approach reduced capital expenditure, shortened installation and commissioning time, and minimised site disruption. Minor electrical upgrades were undertaken, including improved emergency stop provisions and simplified operator controls.

Results & Benefits
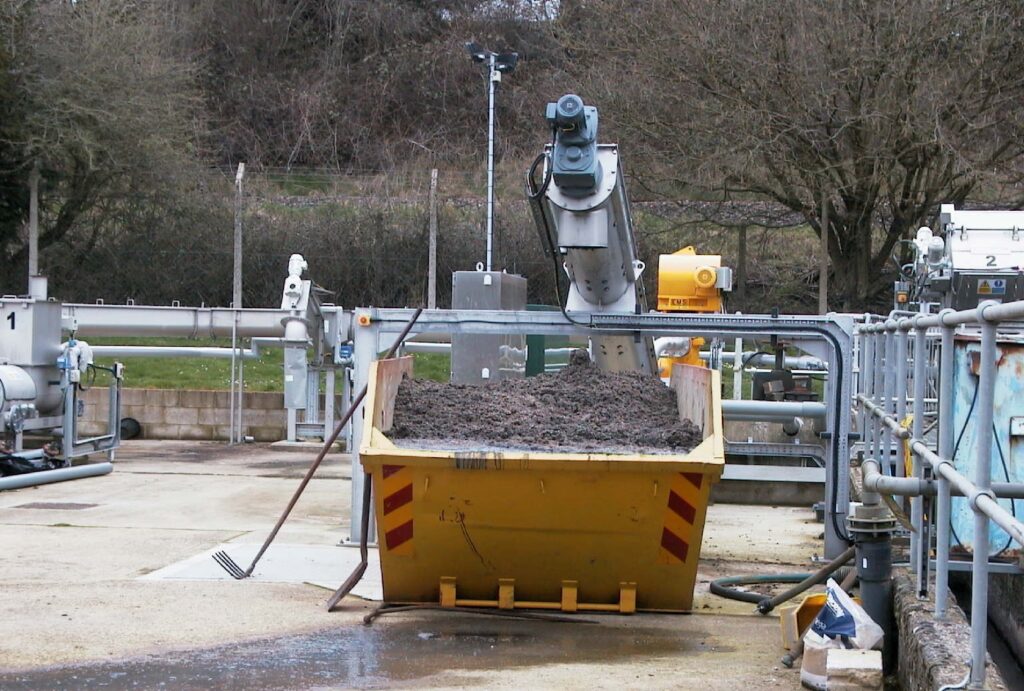
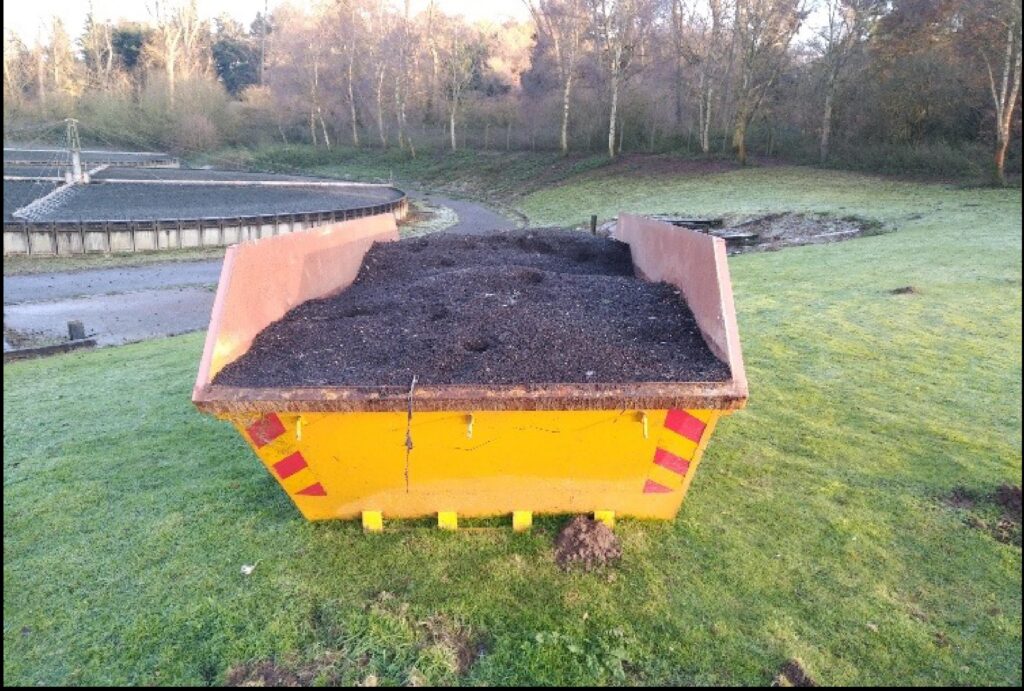
Following commissioning, the system consistently produced full, clean grit skips, confirming effective and reliable grit transfer. Previous blockages and impeller-related failures were eliminated, leading to a significant reduction in maintenance requirements and downtime. Restored pumping reliability allowed the grit classifier to operate at optimal efficiency, reducing grit carryover and downstream equipment wear. Operator safety was enhanced through improved access and reduced interaction with confined spaces.

GRS Strategy Outcomes
The upgrade strongly aligned with GRS strategy principles. Reliability was improved through robust pump design capable of operating in highly abrasive conditions. Efficiency gains were achieved by maximising the performance of existing assets and reducing wear. Safety was enhanced by minimising manual intervention and improving maintenance access. Sustainability objectives were met by reusing existing infrastructure, reducing both waste generation and capital expenditure.

Conclusion
This targeted pump replacement delivered a robust, future-proof grit handling solution with minimal disruption to site operations. The integration of the EMS CVR200 restored reliable operation, reduced maintenance demands, and maximised the value of existing assets, demonstrating how strategic upgrades can deliver substantial operational benefits.

GRIT REMOVAL SOLUTIONS

Background
Recurring failures of the existing grit pump were causing unreliable grit handling, despite the classifier and pipework remaining in good condition. A targeted pump replacement was identified as the most cost-effective solution aligned with GRS strategy principles.

Existing Issues 

  • Reduced pumping efficiency due to impeller erosion
  • Frequent blockages during peak grit loads
  • High maintenance demand and reactive interventions
  • Increased downstream wear from incomplete grit removal

Solution
The upgrade focused on replacing the existing grit pump with an EMS CVR200 Ram Pump while retaining all downstream grit-handling infrastructure. This targeted approach minimised capital cost, reduced waste, and avoided unnecessary disruption to the site, while restoring reliable grit transfer performance.

Why EMS CVR200
The EMS CVR200 Ram Pump was selected for its proven suitability in handling high specific-gravity, abrasive grit slurries. Its adjustable stroke rate allows the pump to respond effectively to variable influent flow conditions. The pump’s abrasion-resistant construction, combined with replaceable wear components, ensures long service life in demanding environments. A low-speed, high-torque ram drive eliminates the need for impellers and other high-wear rotating parts, significantly reducing maintenance. The vertical, top-mounted configuration makes the CVR200 particularly well suited to retrofit installations, with minimal ongoing maintenance requirements.

Installation & Integration
The CVR200 was installed directly on the existing grit chamber footprint, removing the need for civil modifications. Hydraulic integration with the existing classifier and pipework was seamless, ensuring continuity of operation. This approach reduced capital expenditure, shortened installation and commissioning time, and minimised site disruption. Minor electrical upgrades were undertaken, including improved emergency stop provisions and simplified operator controls.

Results & Benefits
Following commissioning, the system consistently produced full, clean grit skips, confirming effective and reliable grit transfer. Previous blockages and impeller-related failures were eliminated, leading to a significant reduction in maintenance requirements and downtime. Restored pumping reliability allowed the grit classifier to operate at optimal efficiency, reducing grit carryover and downstream equipment wear. Operator safety was enhanced through improved access and reduced interaction with confined spaces.

GRS Strategy Outcomes
The upgrade strongly aligned with GRS strategy principles. Reliability was improved through robust pump design capable of operating in highly abrasive conditions. Efficiency gains were achieved by maximising the performance of existing assets and reducing wear. Safety was enhanced by minimising manual intervention and improving maintenance access. Sustainability objectives were met by reusing existing infrastructure, reducing both waste generation and capital expenditure.

Conclusion
This targeted pump replacement delivered a robust, future-proof grit handling solution with minimal disruption to site operations. The integration of the EMS CVR200 restored reliable operation, reduced maintenance demands, and maximised the value of existing assets, demonstrating how strategic upgrades can deliver substantial operational benefits.

Assembled in the USA. Supported Nationwide

USA DISTRIBUTION & SUPPORT...

Contact Us